EPS Molding Technology for Carbon Bike Frames
Every carbon frame is pressed from the inside while it cures. How that pressure is applied decides whether the inner wall comes out smooth and even, or full of wrinkles and resin pools that you cannot see until the frame fails. EPS lost-core molding is one way to solve that problem — and it is the method we use on our most demanding platforms.
A carbon frame has to be pressed from the inside
Laying prepreg into a mould is not enough. Without internal pressure the plies will not compact against the mould wall, and the frame cures with voids, resin-rich pockets and inconsistent wall thickness — defects that are invisible from the outside and that decide where a frame cracks years later.
There are two common ways to generate that internal pressure. The older method is a bladder: an inflatable nylon tube sits inside the layup and is inflated during cure. The newer method is a lost core: a rigid mandrel, shaped to the frame's internal cavity, is wrapped with prepreg, cured inside the mould, and then removed.
| Aspect | Bladder molding | EPS lost-core molding |
|---|---|---|
| How pressure is applied | An inflated nylon bladder pushes the layup outwards against the mould. | A rigid polystyrene mandrel holds the layup in position from the inside while the mould applies external pressure. |
| Inner wall quality | Prone to wrinkles where the bladder creases, especially at tight junctions and bends. | Inner wall follows the machined core surface, so it stays smooth and free of folds. |
| Wall thickness consistency | Can vary where the bladder bridges a corner or where pressure is uneven. | Set by the gap between core and mould cavity, so it is far more repeatable. |
| Resin distribution | Resin can migrate away from high-pressure areas and pool in low-pressure ones. | More even, because the core holds the laminate geometry during the whole cure. |
| Ply movement during cure | Plies can shift as the bladder inflates. | Plies are locked against a rigid core before the mould closes, so the schedule is preserved. |
| Process cost | Lower — fewer steps per frame. | Higher — the core has to be produced, positioned and then removed after cure. |
How EPS lost-core molding works
Core production
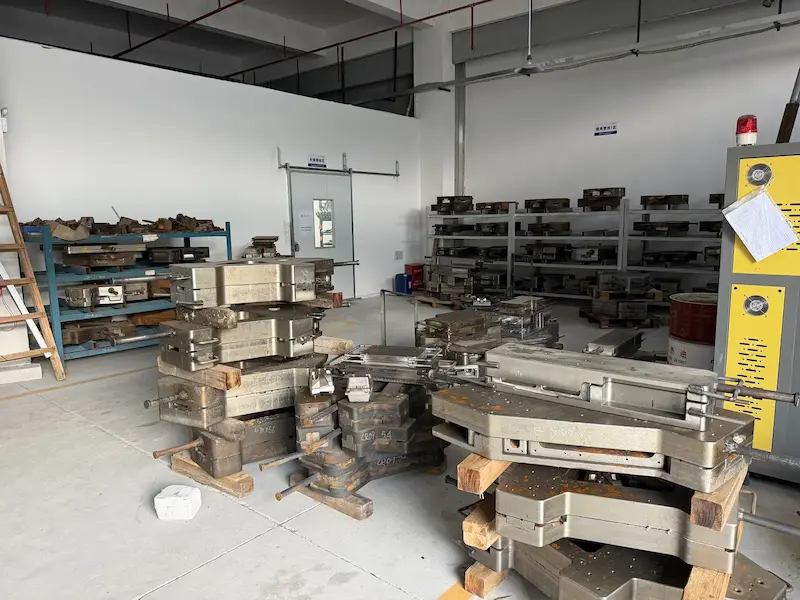
The polystyrene mandrel is produced to the internal geometry of the frame, including the tapered wall thickness the layup schedule calls for. Because the core defines the inside of the frame, its accuracy directly sets the frame's internal accuracy.
Control point: core dimensions checked against the internal cavity drawingLayup onto the core
Cut plies are laid onto the core in the scheduled order and orientation. Because the core is rigid, each ply sits where it is placed instead of sliding, which is what preserves the ply angles through the rest of the process.
Control point: ply count, orientation and overlap verified before closingMoulding and cure
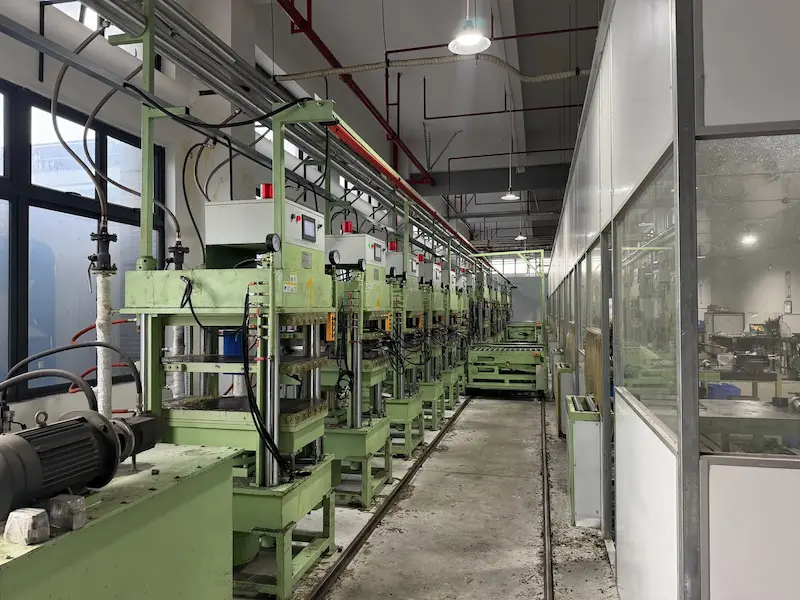
The wrapped core goes into the heated steel mould and is cured under pressure. A defined cure profile controls how the resin flows, gels and finally sets, and therefore how much void content remains in the laminate.
Control point: cure temperature, pressure and dwell time recorded per batchCore removal
After cure, the polystyrene core is collapsed through heat and removed through the frame openings, leaving a hollow monocoque structure with a smooth inner surface. This step is what makes EPS a lost-core process rather than a permanent insert.
Control point: core fully cleared; no residue left inside the frameFinishing and inspection
The frame is trimmed, the bonding surfaces are prepared, and the frame moves into the normal inspection route: dimensional checks, bottom bracket and head tube alignment, and finish inspection.
See quality control for the full inspection listWhy the inner wall matters more than riders realise
The inside of a frame is where stress concentrates. A wrinkle in the inner wall is a resin-rich fold with no fibre running through it, sitting exactly where the load wants to go. It is also invisible, so it survives every visual inspection and only announces itself as a failure.
- Smooth inner walls without bladder creases or folds
- Wall thickness set by tooling rather than by pressure guesswork
- Ply angles preserved because the layup cannot shift during cure
- More even resin distribution, with fewer resin-rich or starved zones
- Reduced internal stress concentration at tube junctions
- Frame-to-frame weight repeatability, which matters for series production
What EPS molding does not solve
EPS is the right answer to a specific problem, and it is not free. Being clear about the trade-offs is more useful to a frame buyer than another list of advantages.
| Limitation | What it means in practice |
|---|---|
| Additional process steps | Core production, positioning and removal all add cycle time per frame, which raises unit cost compared with bladder molding. |
| Tooling and core cost | Both the core and the mould have to be produced to tight tolerance, so the investment is higher and suits platforms that will run in volume. |
| Not a substitute for a good layup | A perfect inner wall cannot rescue a poor ply schedule. EPS improves how well a good schedule is executed; it does not design one. |
| Not a weight saving by itself | The core is removed, so it adds no mass. The benefit is that consistent, defect-free walls make it safe to specify thinner walls, which is where the weight saving actually comes from. |
Where we use it
EPS lost-core molding is specified on our most weight- and consistency-sensitive platforms — including the FM376 all-terrain racing gravel frame and the FM126 super-light aero road frame — and on OEM projects where the weight and consistency target justifies the extra process cost. Molding method is specified per model, so if it matters to your project, ask us to confirm it for the exact frame you are considering rather than assuming it applies across the whole range.
EPS molding FAQ
The material family is the same, the application is not. In frame production the polystyrene is machined or moulded into a precision mandrel that defines the frame's internal geometry, and it is destroyed during removal. It is a tooling element, not a structural part of the finished frame.
Not directly — the core is removed, so it adds no weight. The weight benefit is indirect and more important: because the inner wall is consistent and free of wrinkles, the designer can specify thinner walls with confidence. The saving comes from the layup the process makes possible, not from the process itself.
Ask. Molding method is specified per model, and it is a fair question for any supplier. If a factory cannot answer it, that usually means the process is not under real control. For our own range, contact us with the model you are interested in and we will confirm the method used.
Partially, and by destructive methods only — a frame can be sectioned to reveal the inner wall, which is a normal part of developing a new layup or resolving a problem. In series production the control comes from the process itself: tooling accuracy, ply verification, and a recorded cure profile. See testing and certifications for how finished frames are validated.
Yes, where the volume and the performance target justify the additional tooling and cycle time. It is a project-by-project decision, and we will tell you honestly whether it is worth the cost for your platform. Read more on our OEM services page.
Request EPS molded frame details
If your project depends on internal wall quality, weight repeatability or a specific frame weight, tell us the target. We will tell you which molding method we would use and why.
- Molding method confirmed per model
- Weight repeatability data available
- Reply within one working day